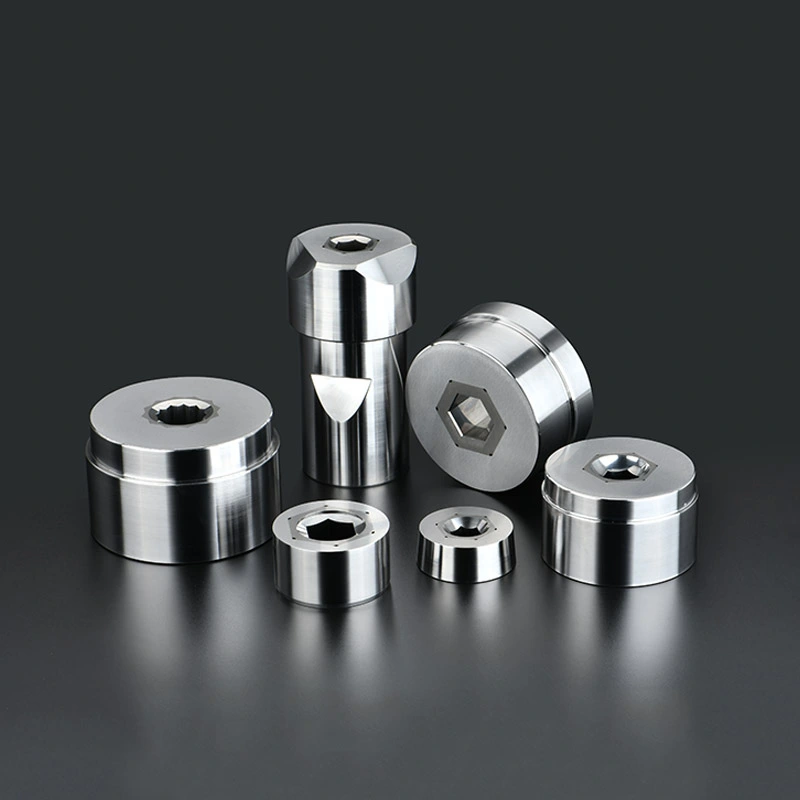
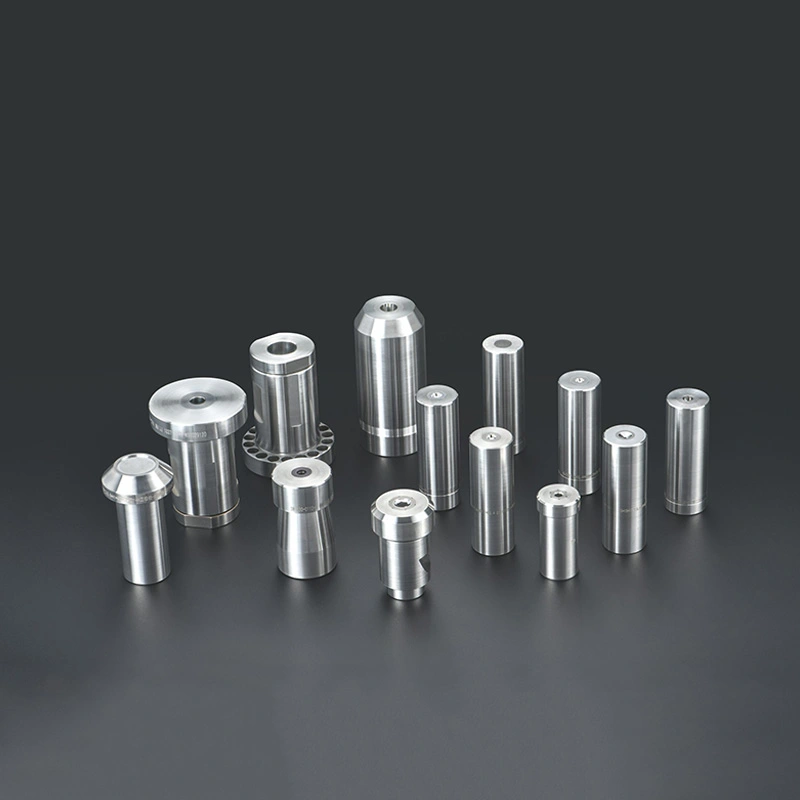
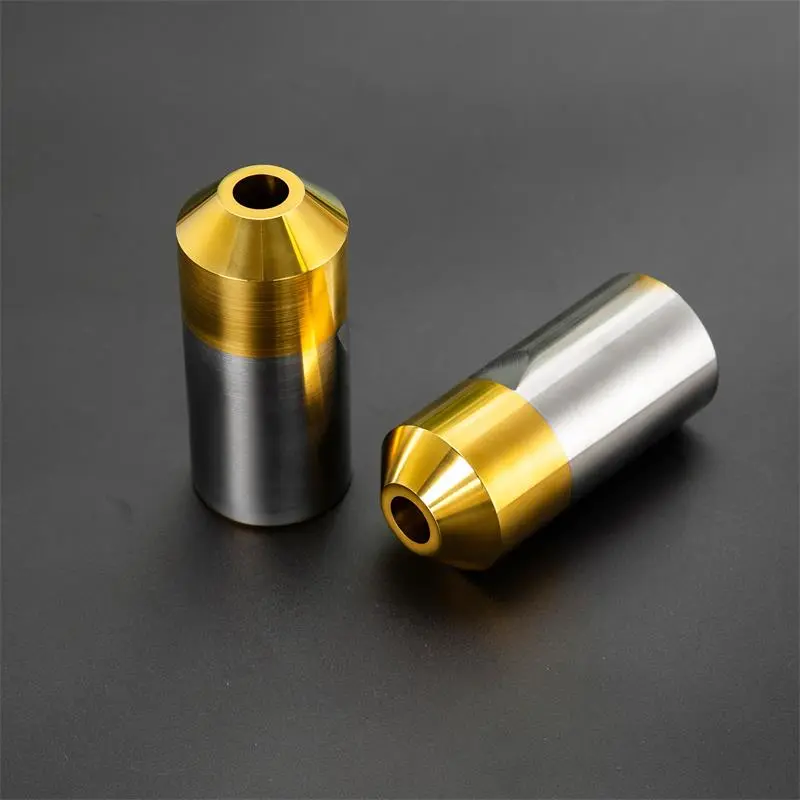
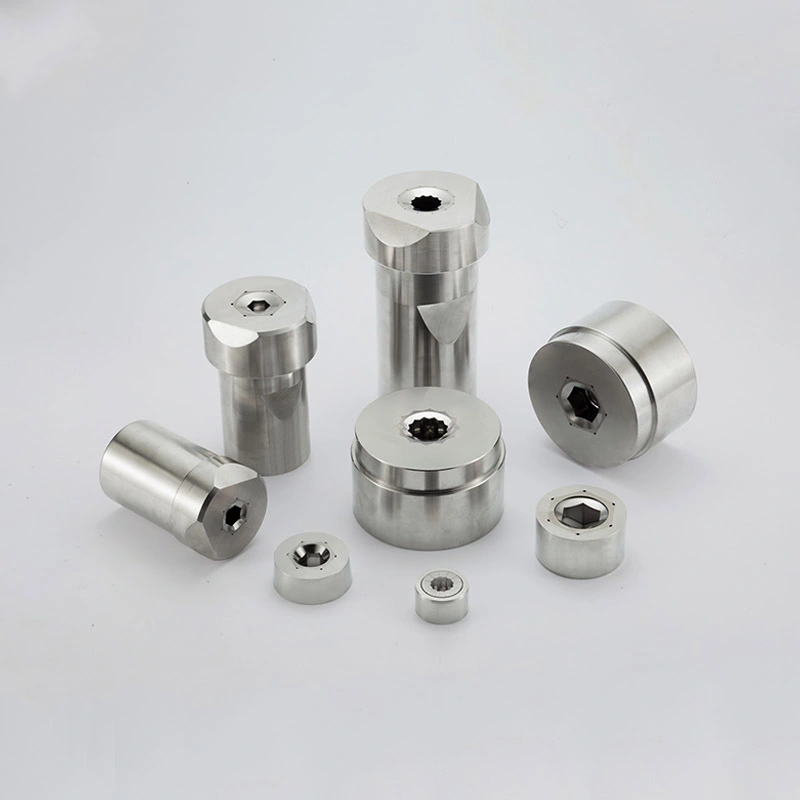
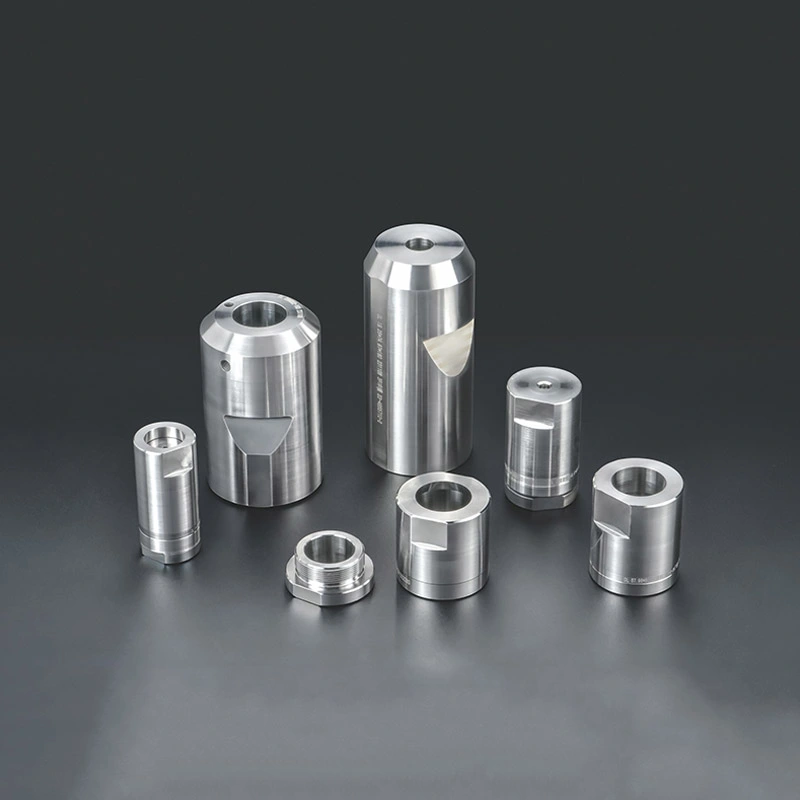
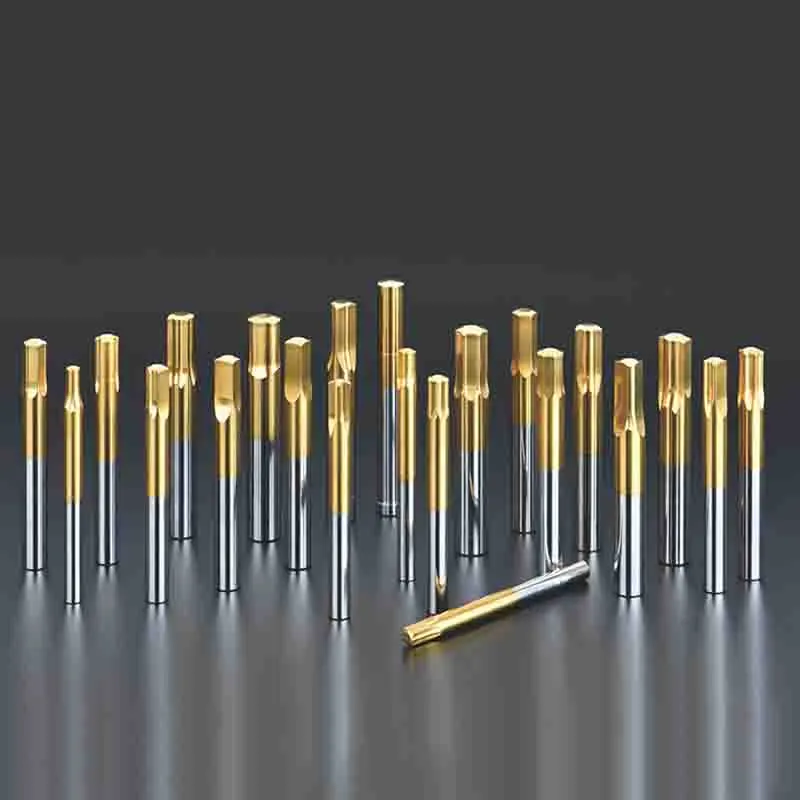
A well-designed cold heading mold must balance dimensional accuracy, compressive strength, impact resistance and wear performance.
Custom cavity profiles are manufactured to match the specified fastener dimensions and forming requirements.
Tungsten carbide and selected tool steels provide material options for different production volumes and forming loads.
Die structures can be engineered to support repeated compressive loads and reduce premature tooling damage.
Die inserts, cases, cavity profiles and related components can be customized for specific forming operations.
Grinding, EDM and polishing help achieve the required surface finish on critical forming surfaces.
Tooling can be manufactured according to supplied drawings, samples and machine installation requirements.
| Parameter | Specification / Options |
|---|---|
| Product Name | Cold Heading Mold |
| Manufacturer | Donglong |
| Place of Origin | Dongguan, Guangdong, China |
| Product Material | Tungsten Carbide, ASP 23, Vanadis Series, CPM REX M4, SKD11, SKD61, HSS, A2, M2, D2, SUJ2, S45C, etc. |
| Tool Steel Options | SKD11, SKD61, H13, ASP23, Vanadis and other grades according to application |
| Dimensional Tolerance | Down to ±0.002 mm on selected critical features, subject to drawing review |
| Surface Finish | Precision grinding and polishing; Ra 0.2 μm may be achievable on suitable features |
| Manufacturing Methods | Grinding, wire cutting, EDM, cnc machining, cnc turning, cnc Milling |
| Surface Treatments | TiCN Coating, TiN Coating, AlTiN Coating, TiCrN Coating, Nitriding, Black Oxide Treatment, and Other Custom Coatings Available upon Request. |
| Standards | Customer drawings and applicable DIN, ANSI, BS or JIS requirements |
| Customization | Material, size, shape, convex and concave marking, coating, laser engraving mark and packing are all customizable. |
| Applications | Screws, bolts, rivets, pins and custom cold-formed partsMachinery Parts and Molds |
Note: Specifications are project-dependent. Hardness, tolerance, coating and surface finish must be confirmed against the selected material, die geometry and customer drawing.
Material composition and physical properties of available carbide grades.
| Grade | WC + Other %, ±0.5% | Co %, ±0.5% | Grain Size | Density g/cm³ | Hardness HRA, ±0.5 | TRS N/mm² |
|---|---|---|---|---|---|---|
| KG5 | 88 | 12 | Medium | 14.31 | 88.3 | 340 |
| KG6 | 86 | 14 | Medium | 14.12 | 87.3 | 320 |
| EA65 | 82 | 18 | Coarse | 13.75 | 85 | 300 |
| EA90 | 76 | 24 | Coarse | 13.22 | 82.8 | 270 |
| ST6 | 85 | 15 | Coarse | 13.8 | 86 | 270 |
| ST7 | 80 | 20 | Coarse | 13.4 | 85.3 | 270 |
| VA80 | 80 | 20 | Coarse | 13.58 | 84 | 280 |
| VA90 | 78 | 22 | Coarse | 13.39 | 82.5 | 240 |
| VA95 | 75 | 25 | Coarse | 13.12 | 81.5 | 220 |
Note: Values are reproduced from the original material specification table. TRS values and units should be verified before publication.
Common tool steel grades, hardness ranges, material characteristics and applications.
| Material | Hardness HRC | Material Features | Typical Applications |
|---|---|---|---|
| H13 | 59–61 | Chromium-molybdenum hot-work tool steel offering hot hardness, abrasion resistance and toughness. | Extrusion dies, forging dies, stamping tools and related tooling. |
| SKD11 | 58–61 | Cold-work tool steel with good wear resistance and dimensional stability after heat treatment. | Drawing dies, cold extrusion dies and first-punch holders. |
| SKD61 | 43–53 | Hot-work tool steel offering resistance to thermal shock, thermal deformation and thermal fatigue. | Hot-work dies, cold heading dies and second-punch holders. |
Note: Hardness ranges are retained from the original table. Actual values depend on material condition and heat treatment; confirm specifications before ordering.
Cold heading is a specialized cold-forming operation. The mold controls material flow and supports the workpiece while the heading punch creates the required deformation.
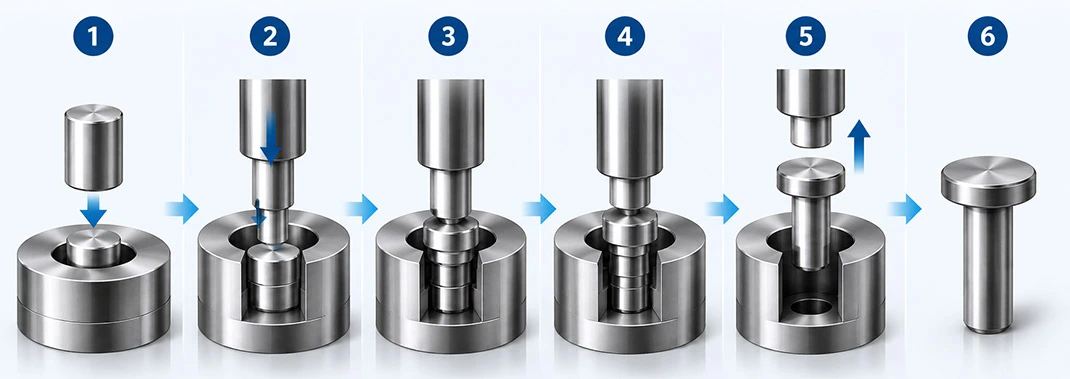
Metal wire or rod stock is fed into the heading machine and cut into the required blank length.
The blank is transferred into the die cavity, which supports and locates the workpiece.
The punch applies compressive force to form the required head, shank or other component features.
Complex geometries may require progressive forming through multiple die stations.
The formed component is removed from the die using the machine's ejection mechanism.
Depending on the part, thread rolling, heat treatment or finishing may follow.
Different forming operations require different die configurations. Donglong supports drawing-based customization for various cold heading tooling requirements.
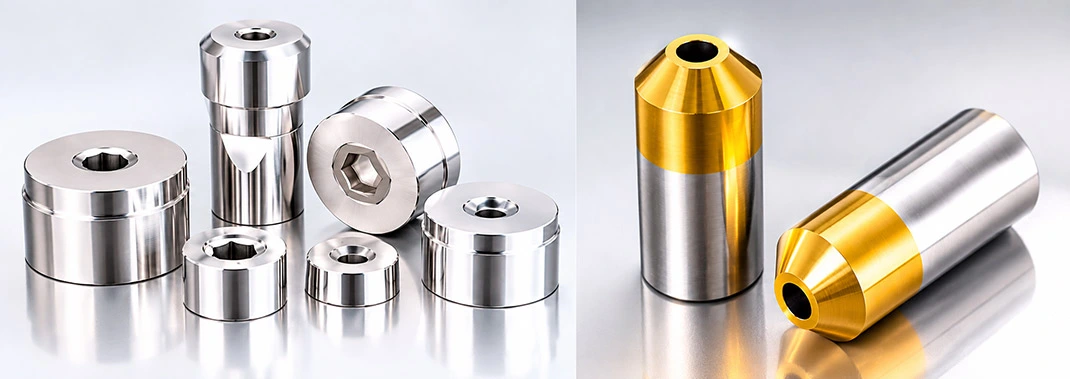
Dies incorporating wear-resistant tungsten carbide inserts for demanding forming applications.
Tool-steel dies selected for applications requiring a balance of toughness and wear resistance.
Custom tooling for progressive forming operations on compatible multi-station heading machines.
Primary forming dies that support the blank and define critical external component geometry.
Split-die structures for selected complex forming and high-load applications.
Drawing-based die solutions for non-standard screws, bolts, pins and special fasteners.
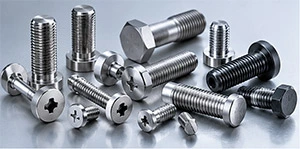
Forming tooling for screw heads, bolt heads, shanks and special fastener geometries.
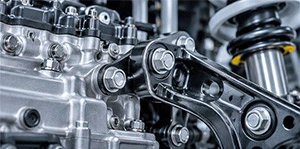
Precision dies for fasteners used in automotive assemblies and mechanical systems.
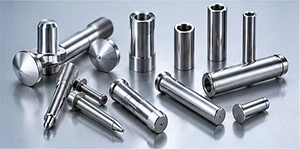
Cold forming dies for rivets, pins and small cylindrical metal components.
Tooling for selected small precision metal parts used in electronic assemblies.
Custom dies for industrial fastening and assembly hardware applications.
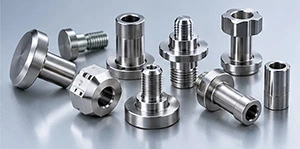
Non-standard tooling for application-specific fasteners and cold-formed parts.
Donglong provides custom cold heading mold manufacturing based on customer drawings, samples and production requirements. Each tooling project is reviewed according to part geometry, machine compatibility, forming loads and material selection.
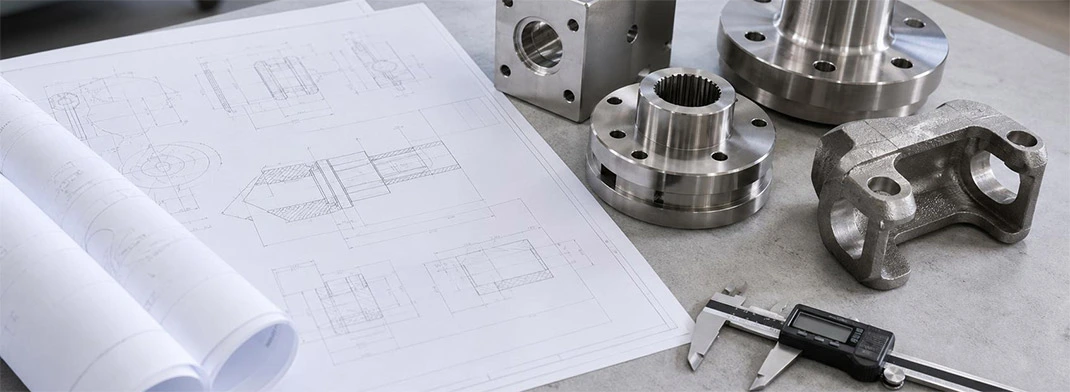
Die cavity profile and geometry
Die insert and case dimensions
Carbide and tool steel grades
Single-stage or multi-stage tooling
Critical tolerances and surface finish
Surface treatment and coating options
Laser marking and packaging requirements
2D drawings or 3D CAD models
Finished fastener geometry
Workpiece material and hardness
Cold heading machine model
Station configuration and tooling dimensions
Expected production volume
Required tolerances and special features
Our team can review your tooling requirements and discuss suitable materials, dimensions and manufacturing methods before quotation.
Request Custom Tooling Quote →The following workflow illustrates the main stages of a typical custom tooling project. Actual operations depend on the die structure, material and inspection requirements.
Evaluate geometry, tolerances, machine compatibility and forming requirements.
Confirm die structure, cavity dimensions and manufacturing specifications.
Select carbide or tool steel according to wear, impact and production requirements.
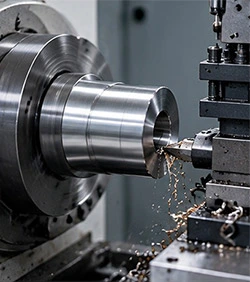
Prepare tooling blanks and perform initial turning or rough machining.
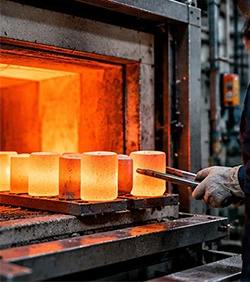
Apply suitable heat treatment to applicable steel components before final finishing.
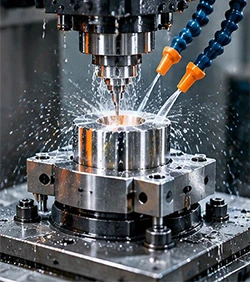
Perform CNC machining, EDM, wire cutting and precision grinding as required.
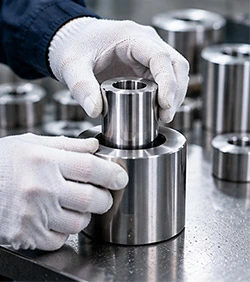
Finish critical surfaces and assemble die inserts and supporting components.
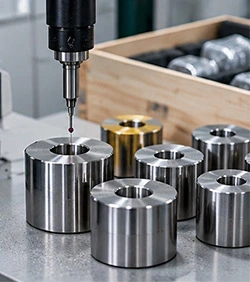
Verify critical dimensions, inspect finish and prepare tooling for shipment.
Cold heading mold performance depends on dimensional accuracy, concentricity, surface quality and material condition. Inspection requirements should be defined according to the customer's drawing and intended forming application.
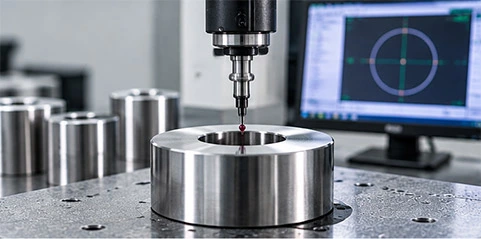
Critical diameters, cavity profiles, lengths, concentricity and other drawing-defined features are checked using suitable measuring equipment.
Material grades and applicable hardness requirements are reviewed against the approved tooling specification.
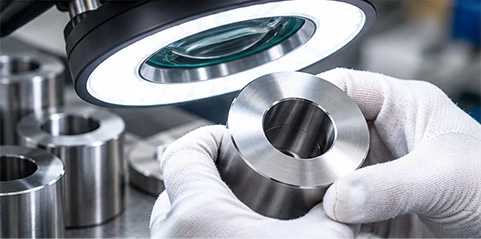
Forming surfaces are inspected for defects, machining marks and specified finish requirements.
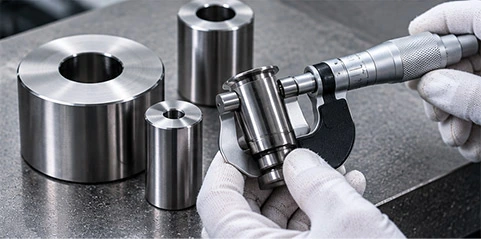
Finished components are checked against approved dimensions and assembly requirements before shipment.
Donglong has focused on precision fastener tooling manufacturing since 1998. Our manufacturing capabilities include CNC machining, EDM, wire cutting, precision grinding and customized cold heading die production.
We support custom fastener tooling projects for automotive, electronics, aerospace, industrial machinery and other manufacturing applications. Our engineering and production teams work with customer drawings to develop practical tooling solutions.
A cold heading mold is a precision tool used with a heading punch to form metal blanks into fasteners and other components through compressive force.
The terms are often used interchangeably in commercial product descriptions. Cold heading die usually refers more specifically to the forming die, while mold may describe the tooling assembly more broadly.
Common options include tungsten carbide, alloy tool steel and powder-metallurgy tool steel. The appropriate material depends on forming pressure, wear conditions and part geometry.
Yes. Donglong supports drawing-based customization for cavity geometry, die dimensions, materials and other tooling requirements.
Donglong lists machining capability down to ±0.002 mm for selected precision features. Achievable tolerance must be confirmed for each drawing and material.
Appropriate material selection, correct die support, suitable lubrication, accurate machine alignment and regular inspection can help reduce premature wear and tooling failure.
Please provide drawings or samples, workpiece material, machine model, required tolerance, tooling quantity and any special coating or surface finish requirements.
Send us your drawings, material specifications, machine details and tooling requirements. Donglong can review your project and provide a customized manufacturing quotation.
For 28 years, Donglong has been focusing on the design, development and manufacture of precision screw molds.


Copyright © 2026 Dongguan Donglong Mold All rights reserved. Privacy Policy